Home/Manufacturing

Capability

Manufacturing

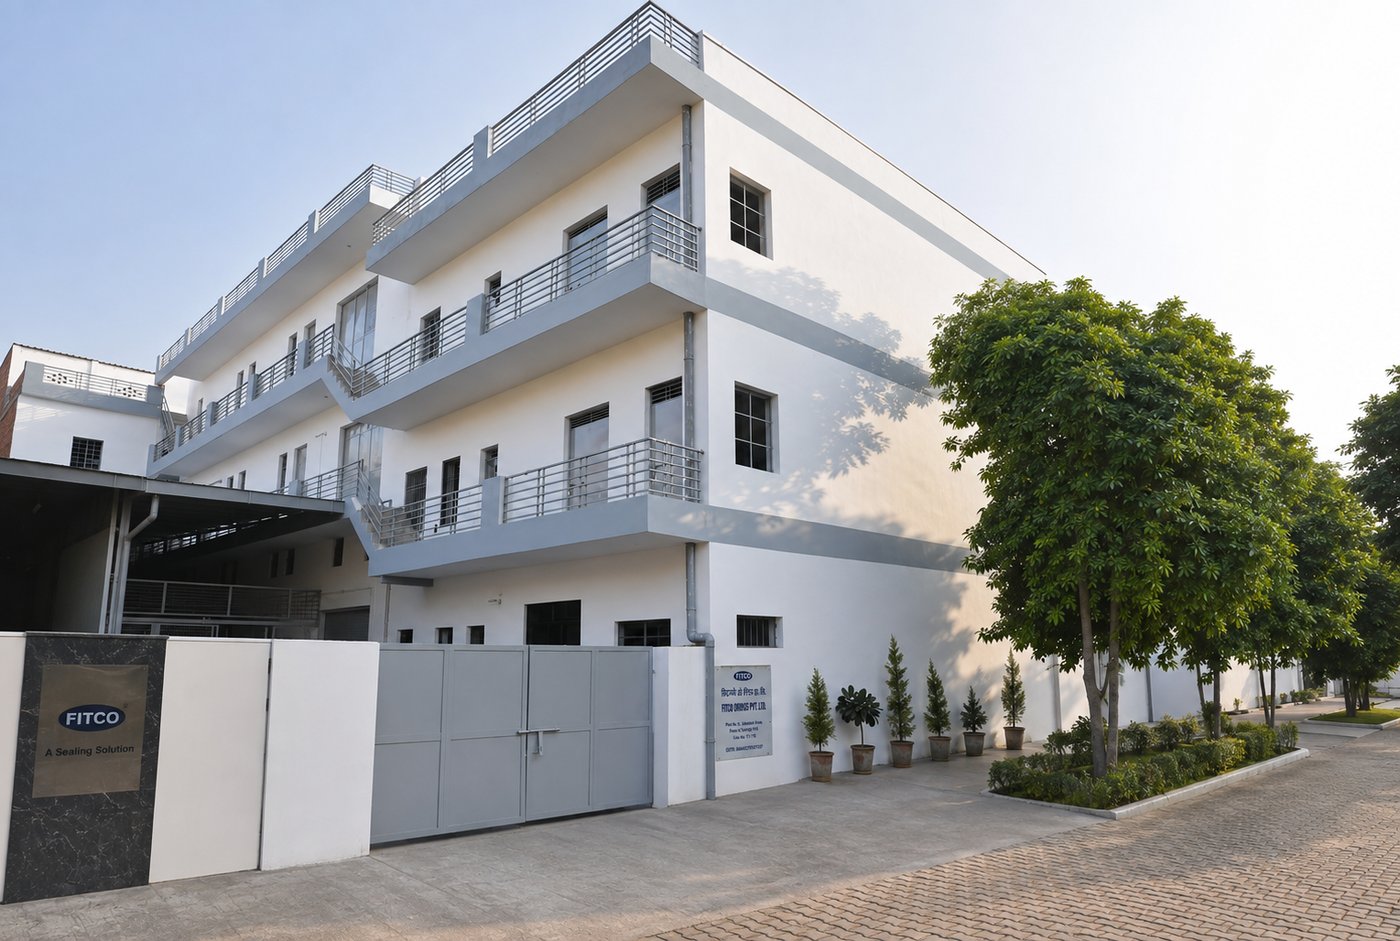
Compounding, tooling, molding, inspection and testing are performed in-house — giving direct control over compound consistency, cure quality and dimensional tolerance across every batch.
ISO 9001:2015Quality Management
ISO 14001:2015Environmental
IATF 16949Automotive QMS
FDA CertifiedFood / Medical

Process

What we do in-house

Process

Compounding

Raw elastomer mixing and compound formulation tuned to hardness, chemical resistance and temperature targets.

View details →
Process

Tooling

Compression, transfer and injection mold tooling design and manufacture for new part numbers.

View details →
Process

Molding

Compression, transfer and injection molding across all core compounds and size ranges.

View details →
Process

Inspection

Dimensional inspection against drawing and standard tolerance classes, batch by batch.

View details →
Process

Testing

Physical property and compound verification testing, including hardness and compression set.

View details →
Process

Prototyping

Low-volume and prototype tooling for design validation ahead of full production commitment.

View details →

Quality Assurance

Built into every step

Quality at FITCO is not a final gate — it is embedded across the entire manufacturing workflow. Raw material batches are tested for Mooney viscosity, specific gravity and cure characteristics (MDR) before release to moulding. In-process controls monitor platen temperature, cure time and press tonnage in real time. Finished parts undergo dimensional inspection on optical comparators, hardness verification on Shore A durometers, and visual inspection under magnification for flash, flow lines and surface defects.

AQL sampling follows ISO 2859-1 at Level II (General Inspection). Full 100% lot inspection is available and standard for safety-critical applications in oil & gas and aerospace. FITCO's laboratory performs tensile testing (ASTM D412), compression set (ASTM D395), ageing and fluid immersion resistance, and ozone resistance tests. External NABL-accredited labs are used for customer-specified third-party validation.

See Quality & Certifications for our full quality-system documentation and certificate details.

Process

Compounding

FITCO operates in-house Banbury mixers and two-roll mills to compound rubber from raw polymer, fillers, plasticisers, curatives and colourants. Each batch is mixed to a verified recipe with Mooney viscosity, specific gravity and cure-rheometry (MDR) tested before release to moulding. In-house compounding gives us direct control over material traceability, lot consistency and the ability to formulate custom compounds to your specific fluid, temperature or regulatory requirements.

Process

Tooling

Our tool room designs and manufactures compression, transfer and injection moulds in-house using CNC milling, wire EDM and surface grinding. Mould cavities are precision-ground to deliver O-ring and seal tolerances to ISO 3601-1 Class A and AS568B standards. Having tooling on-site shortens new-product lead times — prototype tooling is typically ready in 5–10 working days, and production tools in 3–4 weeks.

Process

Moulding

FITCO runs compression, transfer and injection moulding presses from 50 to 500 tonnes, processing all major elastomer families (NBR, FKM, EPDM, Silicone, HNBR, FFKM, CR, ACM, PU and FVMQ). Temperature-controlled platens and automated press-cure timers ensure repeatable vulcanisation. Post-mould deflashing is performed by cryogenic tumbling or manual trimming depending on part geometry and tolerance class.

Process

Inspection

Every production lot is inspected per the control plan — dimensional verification on optical comparators and profile projectors, hardness (Shore A durometer), and visual inspection under magnification for flash, flow lines and surface defects. AQL sampling follows ISO 2859-1 at Level II (General Inspection). Full lot inspection (100%) is available on request and is standard for safety-critical applications in oil & gas and aerospace.

Process

Testing

FITCO's laboratory performs tensile and elongation testing (ASTM D412), compression set (ASTM D395), hardness (ASTM D2240), ageing and fluid immersion resistance, low-temperature retraction (TR-10) and ozone resistance tests. Cure rheometry (MDR per ASTM D5289) and Mooney viscosity (ASTM D1646) are run on every compound batch. External NABL-accredited labs are used for customer-specified third-party validation.

Process

Prototyping

For new-product development and first-article validation, FITCO provides prototype O-rings and seals from single-cavity or multi-cavity sample tools with typical lead times of 7–15 working days from drawing approval. Prototypes are moulded in the production-intent compound so test results are representative of series production. PPAP (Production Part Approval Process) documentation is supplied on request for automotive and regulated-industry customers.

Get a quote on your O-ring or sealing requirement

Send drawings, sizes, materials or an existing part number — our engineering team will respond with pricing, lead time and technical guidance.

Request a Quote Browse Technical Resources